Standards guide · Basics
Tolerances and limit deviations: why they exist and how to read them
On our component pages every dimension states which range the standard allows. This page explains the level below: why these ranges exist at all, how a number gets into a standard – and why “no limit” in a standard can mean three different things. There are no table values here. They belong to the part in question.
Why no dimension works without a range
An elbow with an outside diameter of 114.3 mm never measures exactly 114.3 mm. No manufacturing process hits a number; tools wear, materials spring back, heat expands. That is not a defect but the normal case – and precisely why a standard must say how far reality may deviate from the number.
A dimension without a limit would be doubly useless: not orderable, because the manufacturer does not know what to hit, and not inspectable, because the inspector does not know what to let through. The limit is therefore not a restriction on a promise; it is the promise.
The second reason is interchangeability. When a fitting is welded in, it meets a pipe made to a different standard. For the two to fit together without anyone matching them beforehand, both standards have to apply the same yardstick at the joint – and that is exactly what they do.
Four words that are constantly mixed up
On the shop floor everything is a “tolerance”. In technical language these are four different things, and the difference matters as soon as someone starts calculating:
| Word | What it denotes | Example |
|---|---|---|
| Nominal size | the number that is ordered and drawn | 114.3 mm |
| Limit deviation | the permissible deviation from the nominal size, with sign | −1 % / +1 % |
| Limit sizes | the two sizes themselves that are still permissible | 113.16 to 115.44 mm |
| Tolerance | the distance between the two limit sizes | 2.28 mm |
Why we show limit sizes and not limit deviations: because nobody can read a deviation off a calliper. Whoever measures has a number and wants to know whether it lies between two others – not whether a difference they first have to form lies in an interval they also first have to form. In the drawing the short word “tolerance” is used all the same: it is the word everyone uses, and space on a sheet is precious.
How a number gets into the standard
A limit is always a trade-off between two costs: a tight tolerance makes manufacture expensive, a wide one makes installation expensive. The standards committee places it where usual manufacture holds it without special effort and usual installation tolerates it without rework.
Why large parts get a percentage and small parts millimetres. A fixed millimetre limit would be generous at ⌀ 21.3 and unattainable at ⌀ 1219 – the manufacturing deviation grows with the part. That is why EN 10253 states a three-part rule for the outside diameter:
- ±1 % of the nominal size – the actual statement,
- at least ±0.5 mm – otherwise the percentage rule would fall below what is measurable and manufacturable at small diameters,
- at most ±5 mm – otherwise it would allow gaps at large diameters that no weld can bridge any more.
These three lines are not formula clutter but three different worries, dealt with one after the other. Whoever has seen this once reads every similar rule faster.
The ways of setting a limit
A tolerance is not always a number. We went through the limit deviations of our components, and several different ways came together in which a standard sets a limit:
| Kind | What it means | Example |
|---|---|---|
| symmetrical | the same deviation upwards and downwards | the overall length of a fitting |
| asymmetrical | unequal upwards and downwards – usually because only one direction carries load | the wall thickness, whose lower limit deviation decides the internal pressure |
| proportional | the deviation is a share of the nominal size | the outside diameter at the welding end |
| upper limit | limited on one side only | the out-of-roundness |
| relative limit | the limit is a share of another quantity | the inside diameter at the narrowest point, referred to the connection |
| range | absolute lower and upper limit, without a nominal size | the bevel angle at the welding end |
| multiple | the limit is a multiple of another dimension | the length of a wave on the back of an elbow |
| angle | a limit given as an angle | the inclination of a sealing face |
| in words | a requirement without a number | the ends shall be free from dangerous burrs |
| general tolerance | no value of its own – the general tolerance of the standard applies | dimensions without their own entry |
| contained | no limit value of its own – and yet limited, because another dimension drags the limit along | the roundness at small diameters: the largest and the smallest diameter must each lie within the diameter limit deviation |
| by agreement | the standard expressly refers to the order | the joint preparation for very thick walls |
| none | there is deliberately no limit | the wall thickness of the fitting body upwards – more wall makes nothing worse there |
Counted on the whole rule base for butt-welding fittings and flanges in our data layer; the German page shows the number of rule lines per kind, rebuilt from the data with every change.
The three highlighted ones are the reason for this page. “No limit value” means three different things in a standard, and these three cases are confused every day:
- Contained means: the limit is somewhere else. Below ⌀ 273, EN 10253 names no value of its own for the roundness – but the largest and the smallest diameter must each lie within the diameter limit deviation, and that limits their difference by itself. Whoever reads “no requirement” here reads wrongly.
- By agreement means: the standard considers the case too varied to regulate and expressly pushes it into the order. Whoever agrees nothing here gets what the manufacturer considers right – in accordance with the standard.
- None means: the limit does not exist, and that is a decision. On the body of a fitting the wall thickness is not limited upwards, because a thicker wall makes nothing worse there – it carries more. Downwards it certainly is limited.
Why measurement is stricter at the welding end than on the body
Almost all fitting standards separate two places: the welding end and the body. The tight limits apply at the end, the wide ones or none at all on the body. The reason is simple: the end is where the welding happens. There the fitting meets a pipe, and there it is decided whether the joint fits. On the body the part touches nobody.
That is why the pipe standards of the EN 10216 series say the same sentence for the outside diameter as the fitting standard, word for word. That is no coincidence but intent – what comes together at the joint has to fit together.
What this means at goods inward
- Measure where the standard measures. A diameter measured on the body and held against a limit deviation for the end yields a complaint that is none.
- Roundness needs two measurements in the same cross-section – the largest and the smallest outside diameter. A single value says nothing about it.
- For the wall thickness the lower limit deviation is the one that carries. It decides the permissible internal pressure; upwards, more wall is no defect.
- A non-binding value in a standard is not a promise. It is one solution, not the solution – what governs is the verification the standard provides for it.
Scratches and imperfections in the gasket face – what is acceptable?
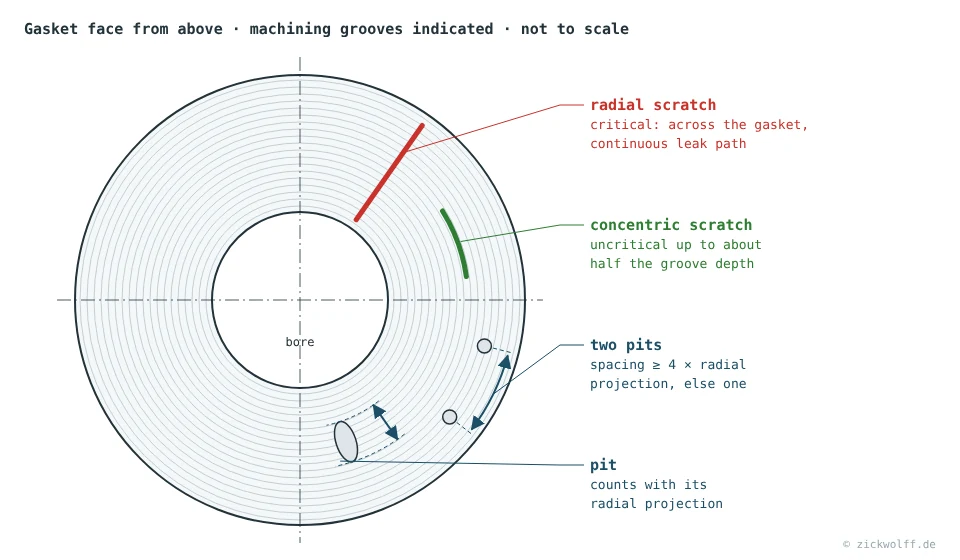
Direction comes first, depth second. A radial scratch – from the bore outwards, across the gasket face – is a continuous leak path under the gasket and is critical even when it is shallow. A concentric scratch runs with the machining grooves and is bridged by the gasket – up to about half the groove depth it is uncritical. Pits count with their radial extent, measured across the grooves. If two lie closer together than four times that extent, they count as one imperfection. Projections above the grooves are never acceptable because they lift the gasket.
For ASME pipe flanges the standard grades the acceptable size of an imperfection in the serrated gasket face by nominal pipe size. What is measured is the radial extent – across the serrations, as the difference between the outer and inner radius of the imperfection, both struck from the centre of the bore.
| Standard | NPS | Not deeper than the bottom of the serrations: radial extent up to | Deeper than the bottom of the serrations: radial extent and depth up to |
|---|---|---|---|
| ASME B16.5 | 1/2–2 1/2 | 3.0 | 1.5 |
| ASME B16.5 | 3 | 4.6 | 1.5 |
| ASME B16.5 | 3 1/2–6 | 6.4 | 3.0 |
| ASME B16.5 | 8–14 | 7.9 | 4.6 |
| ASME B16.5 | 16 | 9.6 | 4.6 |
| ASME B16.5 | 18–24 | 12.7 | 6.4 |
| ASME B16.47 | 26–36 | 12.7 | 6.4 |
| ASME B16.47 | 38–48 | 14.2 | 7.1 |
| ASME B16.47 | 50–60 | 15.7 | 7.9 |
Large-diameter flanges to ASME B16.47 (NPS 26 to 60): values taken from a manufacturer reference – the check against the standard itself is still pending.
In addition
- Two imperfections must be at least four times the largest acceptable radial extent apart.
- Imperfections shallower than half the depth of the serrations are no reason for rejection.
- Projections above the serrations – a burr or raised material – are not acceptable.
- The grades apply to raised faces and large male/female faces. Ring-type joint flanges have their own requirements for the groove flanks.
- The reference is the standard serrated gasket face (concentric or spiral, Ra 3.2 to 6.3 µm).
And for EN pipe flanges?
EN 1092-1 has no table of imperfections. It specifies roughness ranges per facing type (Ra 3.2 to 12.5 µm for types A, B1, E and F, Ra 0.8 to 3.2 µm for B2, C, D, G and H) and has them assessed by comparison with reference specimens.
Whether a scratch is acceptable is decided in the EN world not by a product standard but by the gasket and the assembly: gasket manufacturers’ installation instructions and qualification to EN 1591-4 call for gasket faces without radial grooves and scratches, and many operators adopt the grades of ASME PCC-1 Appendix D for figures in their works specifications. The direction rule applies here in exactly the same way.
Repair by welding is permitted by EN 1092-1 only with the purchaser’s written consent and must be stated in the inspection document. A repaired area is assessed to EN ISO 5817, quality level C. A flange repaired by welding without this note is a reason for complaint.
Basis: ASME B16.5-2025 and EN 1092-1:2018 as test reference – statements about the standards, no standard text. Approval in an individual case is given by the manufacturer or by the purchaser with their specification.
Where the limit deviations of our parts are
For every size, with a dimensional drawing and the permissible range for every dimension: our dimension tables for elbows, tees, reducers and caps to EN 10253-2, each with its sister page for stainless steel to EN 10253-4 (elbows, tees, reducers, caps and dished ends). Further tables in English:
Frequently asked questions
Which tolerances apply to flanges, pipes and fittings?
The standard gives a tolerance per dimension - on the component pages the dimensional drawing of each size shows it on the dimension; this page explains what distinguishes nominal size, permissible deviation, limits of size and tolerance and how to read them.
Do you need this fitting?
What you see here, we carry – from stock or to order; what is missing, we find.
Send us what you have – designation, standard, quantity, date. We check the match and availability and get back to you.
Send an inquiryYour inquiry to Zickwolff
Send us what you have – designation, standard, quantity, date. We will clarify the rest with you.
One item or a question
Send inquiry
Not in stock? We procure it – single items too.
Designation, standard and quantity are enough.
Several items
Send bill of materials
200 items? One parts list is enough – we deliver complete.
Attach it as a file.
Helpful if already known: project and country, date needed, certificates, packaging and language of the packing lists. If anything is missing, we will ask.
It is urgent
Request express
When do you need it? Express delivery, to the site if required.
Tell us by when you need the material – we will tell you what is possible.
Technical basis: EN 10253-2 and -4, EN 10216, EN 1092-1 (limit deviations and their wording). All information without guarantee – the current standard texts always prevail. English version September 2026 of the German page.
