Detail page · Gaskets
Gasket installation and bolting: this is where sealing is decided
Experience from training sessions and failure analyses shows: a large share of the problems with flat gaskets do not originate in the material, but in selection, handling and installation. This page walks through the proven installation sequence, explains why bolts are lubricated and the gasket never is – and shows, using typical failure patterns, how to trace failures back to their true root cause.
- Core rule
- build and maintain surface pressure
- Tightening
- cross pattern, in stages
- Lubrication
- bolts yes – gasket never
- Retightening
- only cold
The proven sequence in seven steps – our suggested approach
Overview, not an installation manual: the manufacturer's installation instructions and the plant's requirements always prevail; installing flange connections belongs in the hands of suitably qualified personnel (cf. EN 1591-4).
- Clean and inspect: free the sealing faces of old gasket residue and corrosion, check for scores and damage – scratches running across the face are leak paths.
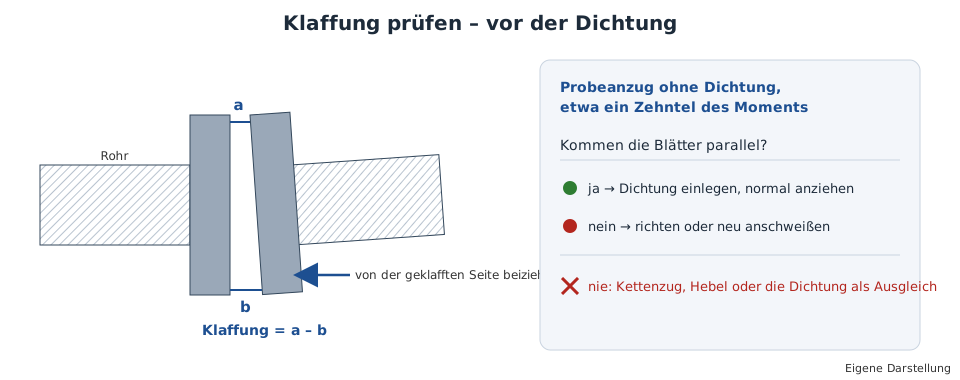
- Align the flanges parallel: the gasket must not be relied on to compensate for misalignment; support the pipework free of stress. If the flange faces gape, pull them up without a gasket at about one tenth of the tightening torque as a trial – only if they come parallel is the gap acceptable (operator guidelines give permissible values in the tenths of a millimetre, graded by nominal size). If the position can only be forced with a chain hoist or lever, the pipe is straightened or the flange re-welded – never compensated with the gasket.
- Place the gasket centred and dry: no adhesive, grease or assembly sprays – the factory anti-stick finish is sufficient. With the IBC form the ring centres itself on the bolts.
- Lubricate the bolts: apply an approved lubricant to the threads and nut bearing faces – bolts, nuts and washers only, never the gasket. Use hardened washers (min. 200 HV): one per bolt, two per stud.
- Tighten in a cross pattern, in stages: seat by hand first, then apply roughly 30 % → 60–70 % → 100 % of the tightening torque, finishing with a control round all the way round at full torque. The tightening sequences by bolt-hole pattern are shown on our page Flange connections and installation.
- Retighten only cold: and for fibre gaskets only as long as the joint has not yet been exposed to a temperature above approx. 100 °C. If the gasket settles, retighten a few hours after assembly or after the first heat-up – cooled down and depressurised. Retightening during hot operation needs its own risk assessment (German TRBS 2141 part 3).
- Thin, simple, single-use: choose the thinnest gasket suited to the flange geometry and duty (manufacturer data prevails – there is no blanket standard thickness), never stack gaskets and never reuse them.
Bolts, nuts, preload
The gasket "lives" on surface pressure – and that comes from bolt preload. Torque is only the aid here: how much preload actually results depends decisively on friction. Dry threads deliver markedly less preload at the same torque than lubricated ones – gasket manufacturers quote 20–30 % less, assembly trials cited in the VCI guideline up to a threefold difference. Torque values therefore only ever apply together with the defined lubrication condition. For critical joints the tightening torque is calculated per connection (gasket parameters to EN 13555 and calculation programs from gasket manufacturers); from large bolt diameters upward, hydraulic tensioning is used, which bypasses the friction uncertainty.
The set includes: bolt material matched to pressure rating and temperature – in the EN system common strength classes or heat-resistant grades, in the ASME system fully threaded studs with two hexagon nuts (standard pairing A193 B7 with A194-2H; stainless steel variants B8/B8M). Number, diameter and length are standardised per flange standard, nominal size and pressure class. From failure-analysis practice: on critical joints, bolts are renewed at every revision – reused, stretched bolts with scattered friction values are a classic cause of failure. And never mix metric and imperial threads on one connection.
Typical failure patterns – and their true causes
"It was the gasket's fault" is the most common misdiagnosis. Four patterns from failure-analysis practice:
- Blown-out gasket: blow-out requires that the surface pressure has fallen below the minimum during operation – typical triggers are pressure surges (for example on start-up against a frozen or closed section of line) or loss of preload. Cause: plant operation or installation, not the material.
- Gasket material in the medium: if a gasket projects uncompressed into the flow channel, the unsupported edge erodes and migrates into the product. Cause: design or an incorrect cut-out – the remedy is a precisely fitted cut-out or a more abrasion-resistant material.
- Gasket destroyed during installation: stacked or glued gaskets (adhesive solvents lower the sustainable pressure), one-sided overpressing due to non-parallel flanges or a missing cross pattern.
- Leak despite the "correct" torque: reused bolts, dry threads, scattered friction values – the preload was never where the torque suggested it was.
For claims handling this means: before replacing the gasket, always check the operating history (pressure surges? temperature?), the installation record (torques, sequence, lubrication) and the condition of the flanges and bolts – otherwise the new gasket fails for the same reason.
Checking, documenting, dismantling – what operator guidelines additionally require
In process plants, flange assembly is a regulated procedure: the German VCI guideline on the assembly of flange connections (Verband der Chemischen Industrie, 2011, for metallic flanges at ambient temperature and without pressure) defines who assembles, how joints are checked and what must be documented. The key points in our own summary – a useful yardstick for plants outside the chemical industry too.
The bolt pattern
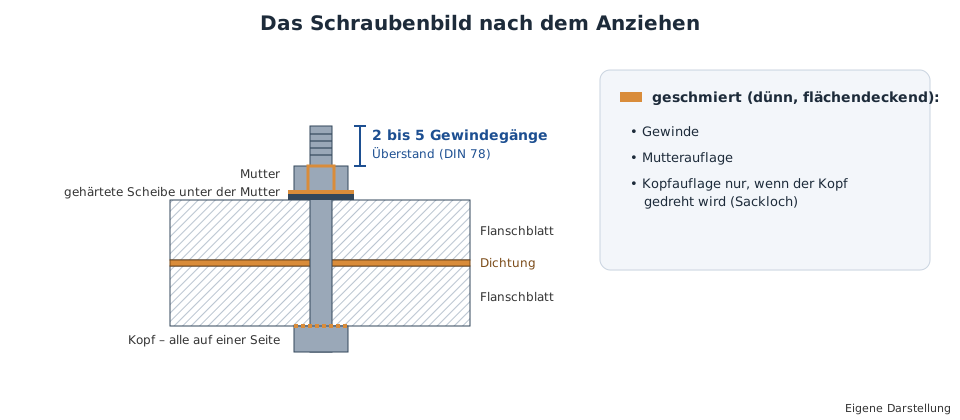
- After tightening, two to five threads protrude beyond the nut (DIN 78); with threaded rods roughly the same on both sides.
- All bolt heads on one side of the flange; on horizontal flanges insert the bolts from above; heads, nuts and washers sit flat.
- Hardened washer under the nut – if the head is turned (blind hole), under the head. Stiff bolts are replaced, not forced.
- Lubricate all sliding surfaces thinly and completely: thread, nut bearing face and, if the head is turned, the head bearing face. Above 250 °C operating temperature use heat-resistant pastes; for oxygen only lubricants approved for it.
- Fit gaskets dry, unkinked and within their shelf life – do not expose fibre and elastomer gaskets to sunlight or heat for long.
Checking and documenting
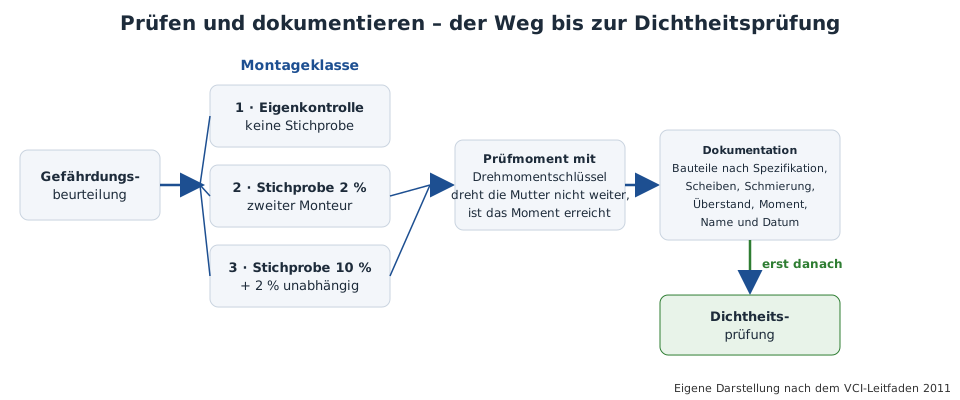
How much is checked is set by the risk assessment through an assembly class: for pipework without special requirements, self-inspection is enough; pipework subject to inspection under the German industrial safety ordinance or the TA Luft air-quality rules gets a spot check by a second fitter (two or ten percent of the joints), and the highest class an additional counter-check by an independent person. The check is made with the torque wrench set to the check torque: if the nut does not turn further, the torque has been reached. If a spot check deviates, the scope is widened. The check comes before the leak test. Documented as a minimum: components to specification (flange with material and PN rating, bolts and nuts with material, gasket), washers present, bolts lubricated, thread protrusion, minimum torque achieved – with name, date and signature.
We deliberately do not quote tightening torques. Tabulated values from operator guidelines apply only under their boundary conditions (flange and bolt material, lubrication, gasket group, tightness class) and must be validated by the operator; outside them the torque is calculated to EN 1591-1 with gasket parameters to EN 13555 – gasket and bolt manufacturers provide programs for this.
Dismantling
- First the release from operations: plant depressurised and flushed, site safety rules observed.
- Secure internals and attachments that are not supported separately before loosening.
- Loosening starts on the side facing away from the body and proceeds crosswise – if the line is under stress, it can spring when released.
- Remove the old gasket completely without damaging the sealing face; never refit used gaskets.
To print for each joint: Flange joint installation checklist – components, installation steps, inspection scope, documentation and dismantling to tick off.
Frequently asked questions on installation and bolting
Why must the gasket itself never be greased?
Lubricant on the sealing face drastically lowers the maximum surface pressure the gasket material can withstand – the gasket is destroyed at a normal tightening torque or creeps out of the joint under operating load. Only the bolt threads and nut bearing faces are lubricated, so that a reproducible preload results from the tightening torque. Many gaskets carry a factory anti-stick finish; additional release agents are only permitted in justified individual cases.
How should flange bolts be tightened correctly?
Always in a cross pattern and in stages: seat all bolts by hand, then apply roughly 30 percent, 60 to 70 percent and 100 percent of the tightening torque over several passes, finishing with a control round all the way round at full torque. This builds up the surface pressure evenly and keeps the flanges from tilting. For critical joints an additional control pass is worthwhile, because the bolts settle after the first tightening.
May a flange connection be retightened while hot?
As a rule, no. Retightening is only done cold – and for most fibre gaskets only as long as the joint has not yet been exposed to a temperature above roughly 100 degrees C, because otherwise the material has already embrittled and breaks on retightening. Hot retightening can destroy the gasket that has already set and is a common trigger for leaks right after start-up.
Which bolts and nuts belong on a flange connection?
In the EN system, common sets use hexagon bolts or studs with matching nuts according to pressure rating and temperature; in the ASME system, fully threaded studs with two hexagon nuts are standard (typically A193 B7 with A194-2H nuts). These are combined with hardened washers (at least 200 HV) – one under each nut, and on studs on both sides. The number, diameter and length of the bolts are standardised per flange standard, nominal size and pressure class. On critical joints, bolts are renewed at every revision.
Why does the connection still leak even though the torque is right?
Torque is only an aid – what matters is the bolt preload, and that depends heavily on friction. The same newton-metres produce 20 to 30 percent less preload with a dry thread than with a lubricated one. Other typical causes: a reused gasket or bolts, uneven tightening without a cross pattern, non-parallel flanges, damaged sealing faces, or a gasket wrongly chosen for the operating conditions. Torque values therefore only ever apply together with the defined lubrication condition.
How many threads must protrude beyond the nut?
Two to five threads (DIN 78) – with fewer, the thread is not fully engaged; with many more, the bolt was chosen too long and heads and nuts often no longer sit flat. With threaded rods the protrusion should be about the same on both sides. The protrusion is one of the items checked and documented in the spot check according to the VCI guideline.
More detail and our range
Gaskets, bolts and flanges from a single source – matched to each other rather than sourced separately.
Your inquiry to Zickwolff
Send us what you have – designation, standard, quantity, date. We will clarify the rest with you.
One item or a question
Send inquiry
Not in stock? We procure it – single items too.
Designation, standard and quantity are enough.
Several items
Send bill of materials
200 items? One parts list is enough – we deliver complete.
Attach it as a file.
Helpful if already known: project and country, date needed, certificates, packaging and language of the packing lists. If anything is missing, we will ask.
It is urgent
Request express
When do you need it? Express delivery, to the site if required.
Tell us by when you need the material – we will tell you what is possible.
Technical basis: KLINGER technical documentation "Flachdichtungen: Grundlagen, Ausfall und Abhilfe, richtige Montage" (2018, presented at Zickwolff) – key statements in our own wording – plus standards facts on EN 13555, ASME B16.5, ASTM A193/A194 and trade articles; checking, documentation and dismantling after the VCI guideline on the assembly of flange connections in process plants (Verband der Chemischen Industrie, August 2011) in our own summary. All information without guarantee – tightening torques must always be determined per connection from manufacturer data; the current standards and technical documentation always prevail.
We supply this material – availability, delivery options and inquiry on the supply page →
